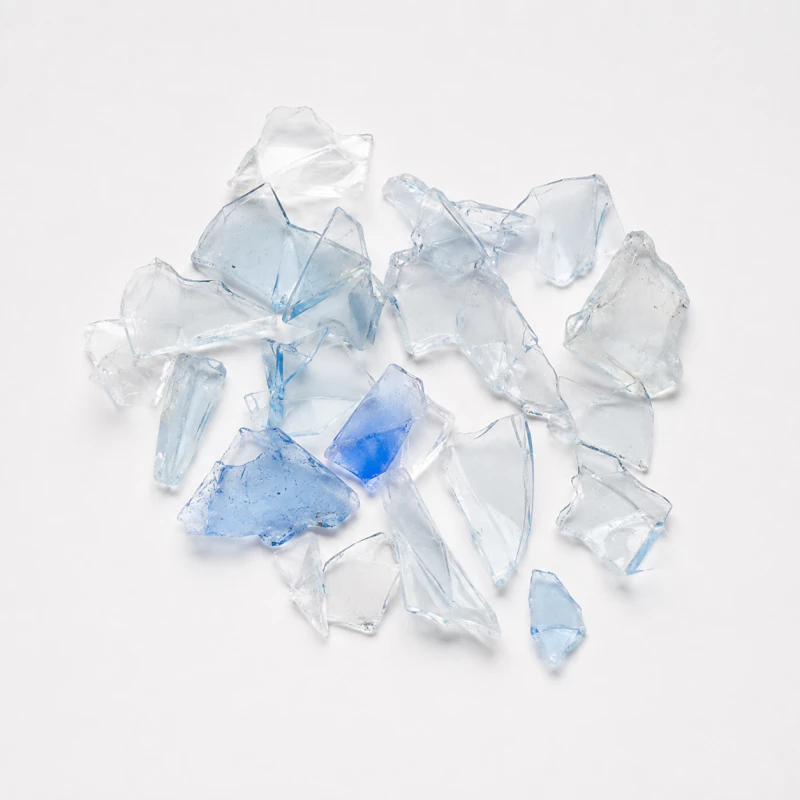
What Is a PET Flake Sorting Solution?
A PET flake sorting solution is a material purification process designed to improve the quality of recycled polyethylene terephthalate (PET) flakes before extrusion, pelletizing, or other downstream processing. Rather than relying on a single machine, the solution combines appropriate material preparation, optical sorting, contaminant removal, and quality control according to the condition of the incoming flakes and the requirements of the finished product. Its primary objective is to separate unwanted colors, non-PET plastics, and other detectable impurities while preserving as much usable PET as possible.
After post-consumer PET bottles are collected, sorted, shredded, washed, and dried, the resulting flakes may still contain clear, light blue, green, and other colored PET, together with PVC, PE, PP, label fragments, and occasional foreign materials. The exact contamination profile depends on the collection stream, bottle preparation, washing process, and previous sorting stages. A properly designed PET flake sorting solution addresses these remaining quality issues and helps recycling plants produce a more consistent material stream for their intended market.
The appropriate configuration depends on whether the plant needs to improve color consistency, reduce non-PET contamination, or achieve both objectives. A color-focused process may be sufficient for relatively clean flakes with limited polymer contamination, while a more demanding recycling application may require separate polymer identification, additional cleaning, and supplementary inspection equipment. The solution should therefore be developed around representative feedstock samples and measurable output requirements rather than assuming that every PET recycling line needs the same equipment configuration.
What Problems Does PET Flake Sorting Solve?
Washed PET flakes can appear clean while still containing small particles that affect the quality of recycled material. Some impurities are visible through differences in color, shape, or surface appearance, whereas other plastics may resemble PET closely enough to require material identification technology. If these particles enter the next processing stage, they can contribute to discoloration, inconsistent processing behavior, or defects in the finished product. PET flake sorting provides an additional purification step to address contaminants that remain after upstream separation and washing.
The main challenges vary between recycling plants. A facility producing clear PET flakes may prioritize colored PET and visible foreign particles, while a plant processing mixed bottle flakes may also need to reduce contamination from other polymer types. Feedstock that contains excessive labels, dust, moisture, or overlapping flakes can create further difficulties because the sorting system needs to identify individual particles under suitable detection conditions. Identifying these challenges before equipment selection helps determine whether the line needs improved preparation, optical color sorting, polymer-based separation, or a combination of these approaches.
| Sorting Challenge | Recommended Solution Approach | Expected Process Benefit |
|---|---|---|
| Mixed clear, blue, green, and other colored PET flakes | Optical color sorting configured for the target color grades | More consistent color composition in the accepted material stream |
| PVC or other unwanted polymer flakes | Suitable polymer-identification sorting, such as NIR where applicable | Reduced contamination by detectable non-target plastics |
| Labels, opaque particles, or visually different foreign materials | Improve washing and screening, then select optical or supplementary separation based on the contaminant | Cleaner feedstock and fewer avoidable sorting difficulties |
| Unstable feed distribution or overlapping flakes | Optimize screening, drying, metering, and single-layer presentation | More reliable particle detection and ejection |
How Does a PET Flake Sorting Solution Work?
A complete PET flake sorting process starts with feedstock assessment and preparation, followed by the separation stages selected for the material. The aim is to present flakes consistently to the detection system, identify unwanted particles using suitable sensors, and remove those particles without unnecessarily rejecting valuable PET. The exact process sequence depends on the existing recycling line, the cleanliness of the washed flakes, and the specifications required by the next production stage.
Feedstock Preparation and Flake Distribution
Before optical sorting, the flakes should be prepared to suit the selected equipment. Washing and drying help reduce residual dirt, moisture, and surface contamination, while screening can remove fines and separate material outside the intended size range. A controlled feeding system distributes flakes toward the detection area so that the particles are presented as consistently as practical. Excessive overlap, dust, or inconsistent feeding can interfere with detection and reduce effective sorting performance, so upstream preparation is an important part of the overall solution.
Color Identification and Separation
When the main objective is to separate PET by color, an optical color sorter analyzes the appearance of individual flakes under controlled illumination. The system compares detected color characteristics with the selected sorting criteria and activates pneumatic ejectors to remove flakes classified as unwanted. For example, a plant producing clear PET flakes may configure the sorting stage to reject green, blue, or other colored particles, depending on the incoming material and the required output grade. The target colors and rejection settings should be confirmed through material testing because transparent flakes, irregular surfaces, lighting conditions, and mixed color shades can affect detection.
Polymer Identification and Contaminant Removal
Color sorting alone cannot reliably distinguish every plastic type. PVC, PE, PP, and other polymer contaminants may have colors similar to those of the target PET flakes, making polymer identification important when material composition is a key quality requirement. Where suitable for the feedstock, near-infrared technology can help distinguish plastics according to their spectral response. Its effectiveness depends on factors such as particle presentation, surface condition, material composition, and sensor configuration, so a sample test is recommended before specifying the sorting stage.
Not every impurity should be assigned to an optical sorter. Metal fragments, dense foreign materials, fine particles, and residual labels may require upstream or downstream equipment selected for their physical properties. For example, metal separation may be more appropriately handled by dedicated metal detection or separation equipment, while washing and screening can address certain surface residues and size-related issues. The complete solution should assign each contaminant to a suitable process instead of expecting one optical sorting machine to remove every type of impurity.
Recommended Process Flow for PET Flake Recycling
The recommended process flow depends on whether the plant is building a new line or upgrading an existing washing and recycling system. In a typical washed-flake purification application, preparation equipment is used to establish a stable feed, followed by one or more sorting stages selected according to the required separation tasks. The line may also include final inspection and quality sampling to verify that the accepted flakes meet the intended product specification.
| Process Stage | Main Function | Key Consideration |
|---|---|---|
| Washing and drying | Reduce dirt, residues, and moisture before optical inspection | The required cleanliness and dryness depend on the sorting equipment |
| Screening and feed preparation | Control particle size and improve the consistency of material distribution | Avoid excessive fines and unstable feeding conditions |
| Optical color sorting | Separate unwanted colors and visually distinguishable particles | Set rejection criteria according to the target PET color grade |
| Polymer sorting, where required | Reduce detectable non-target polymers such as PVC, PE, or PP | Confirm that the selected sensor can identify the actual contaminants |
| Final quality inspection | Check output purity, color composition, and remaining visible impurities | Use representative samples and agreed quality criteria |
These stages do not have to be installed as a fixed sequence in every facility. Some plants already have effective washing, drying, and metal separation systems and only need an optical sorting stage. Others may need to improve feed preparation before adding a sorter, because unstable material conditions can limit the performance of even a well-matched detection system. A line assessment helps determine which stages are necessary and where new equipment will contribute the most value.
Choosing Between Color Sorting and NIR Sorting for PET Flakes
Color sorting and near-infrared sorting address different separation objectives, although they may be used together in a recycling line. A color sorter focuses on visual differences, making it suitable for applications in which the target is to separate clear, blue, green, or other color groups. NIR-based sorting identifies materials through their spectral response and can help distinguish certain polymer types that cannot be reliably separated by color alone. The right choice depends on the impurities present in the feed and the quality requirements of the accepted PET flakes.
| Selection Factor | Optical Color Sorting | NIR-Based Polymer Sorting |
|---|---|---|
| Primary objective | Separate flakes according to detectable color differences | Identify and separate suitable polymer types |
| Typical target | Clear PET versus colored PET | PET versus detectable non-target plastics |
| Main limitation | Similar-looking materials may not be distinguishable by color alone | Performance depends on spectral response, material presentation, and sensor limitations |
| When to consider it | Color consistency is a major output requirement | Polymer contamination is a major concern |
For a feedstock with both color variation and polymer contamination, a combined approach may be appropriate. However, adding more sensors does not automatically guarantee a better result. The equipment must be able to detect the specific contaminants under the actual operating conditions, and the additional stage must justify its effect on recovery, throughput, operating costs, and maintenance. Material trials are the best way to establish whether one sorting stage or multiple stages are appropriate.
Applications of PET Flake Sorting Solutions
PET flake sorting is used in recycling operations that need to improve material consistency before further processing or sale. The required sorting strategy differs according to the target market, the source of the flakes, and the acceptable levels of color and polymer contamination. A solution designed for clear flakes may use different rejection settings from one intended to produce mixed-color material for applications with less demanding appearance requirements.
Bottle-to-Bottle PET Recycling
Bottle-to-bottle recycling places particular emphasis on feedstock quality and control of unwanted materials. A PET flake sorting solution can support this process by reducing detectable colored flakes and non-target plastics before subsequent treatment and manufacturing. However, optical sorting is only one part of a complete recycling process and does not, by itself, establish that the material meets food-contact requirements. Any intended food-grade application requires the appropriate validated processing steps, quality controls, and regulatory compliance for the relevant market.
Polyester Fiber and Textile Production
Recycled PET flakes may be processed into polyester fibers used in textiles, filling materials, and other fiber-based products. For these applications, color consistency and contamination control can help stabilize downstream processing and reduce unwanted variation in the finished material. The required separation level depends on the fiber product, the subsequent color treatment, and the manufacturer's raw material specifications. A sorting solution should therefore be configured around the actual fiber production requirements rather than applying the same rejection settings to every recycled PET stream.
PET Sheet and Thermoforming Material
Manufacturers producing recycled PET sheet or thermoformed products may need consistent color and low levels of foreign polymer contamination to support stable processing and product appearance. Optical sorting can reduce detectable unwanted particles in the prepared flake stream, while polymer identification may be considered where the incoming material contains plastics that resemble PET visually. The complete process must also account for the customer's requirements for intrinsic material properties, contamination limits, and any application-specific compliance standards.
Washed PET Flake Suppliers
Processors that sell washed PET flakes to other manufacturers can use sorting as a quality-control stage before packaging and shipment. Separating unwanted colors or detectable non-PET particles can help suppliers meet customer specifications and reduce variation between batches. The best configuration depends on the incoming flake quality, the agreed acceptance criteria, and the cost of recovering usable material compared with rejecting it. Representative sampling and documented output testing help establish whether the sorting process is meeting the buyer's requirements.
How to Design the Right PET Flake Sorting Solution
Designing an effective solution begins with the material rather than the machine model. Before choosing equipment, the plant should define the feedstock source, particle-size distribution, moisture condition, color composition, and likely contaminant types. The required output should also be clearly defined, including the target color grade, acceptable polymer contamination, recovery expectations, and the quality requirements of the next processing stage. These details form the basis for selecting the necessary sorting technology and determining whether the existing line needs additional preparation equipment.
Capacity should be evaluated under realistic operating conditions. The actual processing rate depends on the machine configuration, the size and shape of the flakes, how evenly the material is distributed, and the amount of contamination that must be removed. A nominal capacity figure alone cannot show whether the line will achieve the desired purity and recovery simultaneously. It is important to ask for a performance evaluation using representative material and to confirm the test conditions, accepted product quality, and reject rate before finalizing the system design.
Integration with existing equipment is another important consideration. The new sorting stage may need to connect with washing and drying equipment, conveyors, screening systems, storage silos, and downstream extrusion or pelletizing operations. Operators should also consider access for cleaning, routine inspection, compressed-air supply where pneumatic ejection is used, and the handling of rejected material. A well-integrated solution should improve material quality without creating unnecessary bottlenecks elsewhere in the recycling line.
| Project Requirement | Information to Confirm |
|---|---|
| Feedstock condition | Flake size, moisture, dust, color distribution, and contaminant composition |
| Target output | Required color grade, acceptable impurities, and downstream application |
| Sorting technology | Whether color detection, polymer identification, or supplementary separation is necessary |
| Operating capacity | Required throughput under the intended feed and output-quality conditions |
| Existing line integration | Available floor space, conveying arrangement, utilities, and reject-material handling |
| Performance validation | Sample-test results, output purity, recovery, reject rate, and operating conditions |
Frequently Asked Questions About PET Flake Sorting Solutions
The following questions address common decisions when adding or upgrading a PET flake sorting stage. Actual performance depends on the feedstock and equipment configuration, so application-specific testing should be used to confirm the proposed solution.
Can a PET flake sorter separate clear PET from colored PET?
Yes. A suitable optical color sorter can be configured to separate detectable color groups, such as clear, blue, and green PET flakes. The available color categories and achievable separation quality depend on the flake appearance, particle presentation, and the required output specification. Testing representative samples helps establish the appropriate sorting settings and the likely level of residual color contamination.
Can a PET flake sorting solution remove PVC contamination?
A suitable polymer-identification sorting stage may help remove detectable PVC flakes from a PET stream. Color detection alone is not sufficient when PVC and PET have similar visible appearances. The effectiveness of an NIR-based system depends on the material's spectral characteristics, surface condition, particle presentation, and the specific sensor configuration. Where PVC contamination is a critical quality concern, testing with representative feedstock is particularly important.
Can one sorting machine remove every type of impurity?
No single optical sorting configuration should be assumed to remove every contaminant. Different impurities may require different detection methods or physical separation processes. Color sorting is useful for visually distinguishable particles, while polymer identification may help with certain plastics. Metals, fines, residual dirt, and other foreign materials may need dedicated separation or improved upstream washing and screening. A complete solution assigns each major contaminant to an appropriate process.
Does PET flake sorting replace washing?
No. Washing and optical sorting perform different functions and are normally complementary. Washing helps remove dirt, residues, and other surface contamination, while sorting identifies and separates unwanted particles that remain in the material stream and can be detected by the selected technology. The correct sequence depends on the recycling line design, but the flakes should be presented in a condition suitable for reliable sorting.
Can a PET flake sorting machine process flakes of any size?
No. Each sorting system has an operating range determined by its feeding mechanism, detection arrangement, and material-handling design. Excessively large flakes, fines, irregular particles, or a broad size distribution can affect presentation and separation performance. Screening the feed to a suitable size range may improve sorting stability. The acceptable particle-size range should be confirmed with the equipment supplier and tested using the actual feedstock.
How can a recycling plant verify sorting performance before purchase?
The most practical approach is to provide a representative sample of the intended feedstock and define the required output quality in advance. The evaluation should record the incoming contamination profile, accepted-material purity, recovery or reject rate, and operating conditions used during the test. If different contaminant types are present, the results should identify which materials were successfully separated and which remain. This allows the plant to compare proposed configurations against its real production needs instead of relying solely on general specifications.
Build a PET Flake Sorting Solution Around Your Material
Improving PET flake quality requires more than selecting a sorter with a high nominal capacity. The most suitable solution considers the condition of the washed flakes, the types of contamination that remain, the desired output grade, and the requirements of the next processing stage. By combining appropriate feed preparation with color sorting, polymer identification where necessary, and clear quality-control criteria, recycling plants can develop a sorting process that is better aligned with their material and production objectives.
Before finalizing a PET flake sorting project, evaluate representative samples and confirm the performance targets with the equipment supplier. A material-based assessment can help determine the necessary sensor configuration, whether additional separation stages are justified, and how the new equipment should integrate with the existing recycling line. This approach supports a practical solution for improving PET flake consistency, reducing detectable contaminants, and preparing recycled material for its intended application.