What Is a Flake Sorting Machine?
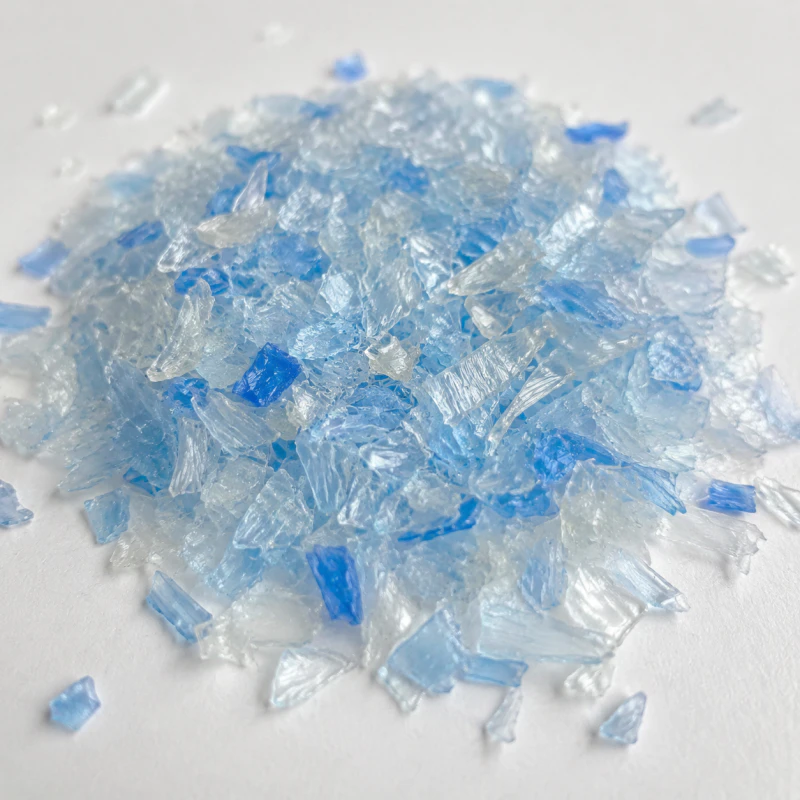
A flake sorting machine is a specialized industrial device designed to automatically separate and categorize plastic flakes based on color, polymer type, and optical properties. Also known as a plastic flake sorter or flake optical sorter, it uses high-resolution cameras and near-infrared (NIR) sensors to scan individual flakes transported on a conveyor belt. A computer vision system then activates precise air jets to eject unwanted flakes, ensuring only the desired material stream continues. This technology has become essential in modern recycling facilities because it transforms mixed plastic waste into high-purity raw materials that can be reused in manufacturing. For example, a typical plastic flake sorting machine can process up to 2,000 kilograms of mixed flake per hour, separating multi-colored polypropylene (PP) flakes from polyethylene (PE) flakes with remarkable accuracy. The machine’s ability to handle varying particle sizes from as small as two millimeters up to twenty millimeters makes it versatile for different post-shredding applications. When integrated with a conveyor system, the flake sorter maintains consistent throughput while reducing manual labor requirements significantly.
The core components of a flake sorting system include a vibratory feeder that creates a uniform monolayer of flakes, a high-speed belt for stable transport, a scanning module housing sensors and cameras, and an array of pneumatic ejection nozzles. The flake optical sorter relies on sophisticated algorithms trained on thousands of flake images to distinguish subtle differences in color shade, degree of transparency, and material composition. In many industrial settings, the plastic flake sorter operates in-line with washing and drying equipment to handle damp or partially wet materials without compromising detection accuracy. Understanding what a flake sorting machine does requires recognizing its role as a quality control gatekeeper—it separates recyclable polymers from contaminants like metal fragments, rubber bits, and wood splinters that could damage downstream processing equipment. Recycling plants worldwide depend on these machines to produce flakes meeting strict purity thresholds for applications like food-grade packaging or automotive components. The evolution from manual sorting to automated flake sorting has drastically improved worker safety by reducing exposure to sharp plastic debris and dust particles.
How Does a Flake Sorting Machine Sort Plastics?
The sorting process combines material handling, optical detection, and pneumatic separation to achieve high-purity results at production speeds. It begins with feeding plastic flakes onto a vibratory feeder that spreads them into a thin, consistent layer. This uniform monolayer is crucial because overlapping flakes can confuse the detection system, leading to misclassification. The flakes, typically ranging from two to twenty millimeters in size, then travel along a high-speed conveyor belt at velocities around two to three meters per second. As they pass under the detection unit, multi-spectral cameras capture reflected visible light while near-infrared sensors measure the unique absorption patterns of different polymer types. This dual-sensor approach enables the plastic flake sorter to identify both visible color variations and molecular composition within milliseconds. For example, the machine can quickly distinguish between a clear PET flake and a frosted PETG flake even though they appear similar to the human eye. The real-time processing power required for this speed means the flake optical sorter relies on industrial-grade computers running dedicated image recognition software.
Once the optical scanning stage identifies a flake as a reject, the computer processor calculates its trajectory and activates specific air jets from a row of precision nozzles arranged across the machine width. These jets release short bursts of compressed air that blow the unwanted flake downward into a reject chute, while acceptable flakes continue unimpeded along their original path to a collection bin. This pneumatic separation mechanism can activate and deactivate individual nozzles hundreds of times per second to handle high throughput rates. After sorting, the accepted material often undergoes a purity check where inspectors or quality sensors verify that contamination remains below one percent. Many modern flake sorting machines incorporate adaptive learning capabilities that adjust sorting thresholds based on real-time feed variations. For instance, if the incoming material contains an unusually high proportion of dark-colored PVC, the system can recalibrate its detection parameters to maintain consistent output quality. The entire cycle from flake detection to ejection completes in under twenty milliseconds, making the process feel almost instantaneous to operators monitoring the machine. Regular calibration checks ensure the pneumatics remain responsive, and the conveyor maintains steady speed to preserve sorting accuracy over extended operating periods.
What Plastics Can a Flake Sorting Machine Detect?
Flake sorting machines can detect a wide range of plastic types, though detection effectiveness varies depending on optical properties and material condition. Among the most successfully sorted polymers are PET, HDPE, LDPE, PP, PVC, PS, and various copolymers such as PETG. These materials align well with the detection capabilities of standard visible light cameras combined with near-infrared sensors. The flake optical sorter excels at separating clear flakes from colored ones, distinguishing white from translucent, and identifying different hue intensities in mixed-color batches. For example, a typical plastic flake sorter can differentiate between a bright red PET flake and a faded magenta PET flake with ninety-nine percent reliability. However, highly opaque black flakes present significant challenges because they absorb large amounts of visible and near-infrared light, making spectral analysis difficult. Advanced polymer sorters equipped with specialized high-power NIR lasers or hyperspectral imaging can partially overcome this limitation, but full detection of black plastics remains an area of ongoing development. Degraded or heavily frosted plastics also create detection difficulties because their surface irregularities scatter light in unpredictable ways, reducing sensor accuracy. Many recycling plants address this issue by prewashing and drying such materials to restore some optical clarity before sorting.
Ultra-thin films with thickness below half a millimeter pose another detection challenge because they tend to wrap around conveyor components or cling together in clusters, preventing the monolayer formation required for reliable scanning. Some flake sorting machines incorporate pre-screening mechanisms like air classifiers to remove these films before they reach the main detection zone. Certain plastic blends, such as multi-layer packaging materials that combine different polymers in a single flake, can confuse detection systems that expect homogeneous material signatures. In these cases, a plastic flake sorter might misclassify the entire flake based on the dominant polymer type. To address this, some facilities combine sequential sorting passes through different machines with varied sensor configurations. The ability to detect common contaminants like aluminum foil fragments, rubber particles, or glass shards varies between models, as these materials produce unique optical responses that some flake sorters are not calibrated to recognize. Despite these limitations, the plastic sorter remains a highly effective tool for most post-consumer and post-industrial recycling streams when operators properly match the machine's sensor configuration to their feed material composition. Prewashing to remove labels, glue residues, and organic contaminants significantly improves detection reliability across all polymer types.
Flake Sorting Machine Specifications
| Parameter | Specification Range |
|---|---|
| Throughput Capacity | 500 kg/h – 5,000 kg/h (depending on flake size) |
| Sorting Width | 600 mm – 2,400 mm |
| Number of Channels | 1 – 6 chute patterns (single or multi-run) |
| Sorting Purity | ≥ 98% – 99.5% (with proper presorting) |
| Power Consumption | 5 kW – 25 kW (including compressed air) |
Beyond these core specifications, practical installation requirements include compressed air supply at pressures ranging from six to eight bar with adequate volume capacity to maintain nozzle responsiveness. The plastic flake sorter's footprint typically measures two to six meters in length and one to three meters in width, requiring dedicated floor space near other material handling equipment. Ambient temperature tolerances range from five degrees Celsius to forty degrees Celsius for most models, making them suitable for both heated indoor recycling halls and covered outdoor installations with climate control. Connection to a central dust collection system is often necessary because the pneumatic ejection process can generate airborne particulates. Maintenance intervals for the optical sensors typically occur every two to four hours in dusty environments, while belt replacement cycles range from six to twelve months depending on operational intensity. Modern flake sorting machines include integrated diagnostic interfaces that display real-time purity percentages, throughput rates, and sensor health metrics on a touchscreen panel, enabling operators to monitor performance without manual sampling.
Flake Sorting vs. Whole Bottle Sorting
Both flake sorting and whole bottle sorting serve distinct roles in plastic recycling, with each method demonstrating advantages depending on the application and desired output quality. Flake sorting provides higher precision for mixed-color or multi-polymer streams because the reduced particle size allows sensors to examine a larger surface area proportionally, leading to more reliable material identification. This method is particularly effective for post-shredding applications where flakes become uniform in shape and size, enabling the plastic flake sorter to detect subtle color variations that would be invisible on larger objects. The energy efficiency of flake sorting on a per-kilogram basis often surpasses that of whole bottle sorting because the flake optical sorter uses less compressed air per unit of sorted material, given the smaller volume of each rejected piece. However, whole bottle sorting remains faster for bulk pre-sorting because it processes entire containers without requiring the energy-intensive shredding step. A whole bottle sorter can handle up to ten tons per hour in some configurations, though its accuracy for small contaminants like caps or labels typically only reaches ninety to ninety-five percent purity.
When comparing contaminant removal effectiveness, the flake sorting machine generally achieves excellent results due to its ability to isolate individual flakes containing embedded impurities. Whole bottle sorters often struggle with small stickers or shrink sleeves wrapped around containers, but flake sorters can reliably eject these after shredding exposes the foreign material. The best scenario for implementing a flake sorting system is when the recycling operation requires post-shredding high purity, such as producing PET flakes for bottle-to-bottle recycling or creating PP flakes for food-grade packaging. In contrast, whole bottle sorting makes the most sense for pre-shredding stages where reducing volume and removing obvious contaminants like metal cans and glass bottles is the priority. Many modern recycling facilities combine both methods in a two-step process: initially using whole bottle sorters to remove large non-plastic items, then passing the shredded material through a plastic flake sorter to achieve final purification. This complementary approach maximizes overall recovery rates while maintaining the high-quality standards demanded by end users. The choice between the two technologies ultimately depends on the specific input material, desired output purity, and the trade-off between throughput speed and sorting precision.
What Industries Use Flake Sorting Machines?
Plastic recycling plants represent the primary adopters of flake sorting technology, using these machines to separate post-consumer bottles, caps, and packaging flakes into single-polymer streams suitable for downstream processing. These facilities commonly process incoming mixed bales containing PET, HDPE, and PP from municipal recycling programs, relying on the plastic flake sorter to achieve purity levels exceeding ninety-nine percent. Packaging manufacturers also frequently integrate flake sorters into their operations to reclaim in-house scrap generated during extrusion or injection molding processes. When producing multi-colored containers, one manufacturing run may create significant quantities of mixed-color waste that, without sorting, would become low-value rejects. The flake optical sorter enables these producers to reintroduce clean, color-sorted regrind into their material flows, reducing raw material costs and environmental impact. Waste management facilities have increasingly deployed polymer sorting machines to handle complex waste streams like electronic waste plastic components and automotive shredder residue. For instance, e-waste recycling contains a diverse mixture of ABS, polycarbonate, and flame-retardant plastic flakes that require precise separation to meet strict hazardous material regulations.
Food-grade recycling lines represent a demanding application for flake sorters because they must produce transparent PET flakes free from colored contaminants and foreign polymers to satisfy safety standards for bottle-to-bottle recycling. In this context, the plastic flake sorter often operates in combination with metal detectors and wash lines to achieve the lowest possible contamination levels. Textile and fiber producers have also adopted flake sorting machines to clean polyester or nylon flakes destined for fleece production or carpet manufacturing. These applications benefit from the machine's ability to remove dark-colored flakes that would otherwise create unsightly specks in final textile products. The automotive industry uses flake sorters to recycle post-industrial plastic components like dashboard trims and bumper covers, separating them by polymer type for remanufacturing. Small and medium-sized recycling entrepreneurs increasingly invest in compact, plug-and-play flake sorting modules that handle capacities between 500 and 1,000 kilograms per hour, enabling them to upgrade their processing capabilities without massive capital expenditure. The widespread adoption across these diverse industries reflects the flake sorters' ability to transform low-value mixed plastic waste into high-purity raw materials that command premium prices in secondary material markets.
How to Choose the Right Flake Sorting Machine
Selecting the optimal flake sorting machine requires a systematic evaluation of feed material characteristics, throughput requirements, and detection capabilities. Begin by analyzing your input material to determine the typical flake size distribution, which should fall within two to twenty millimeters for maximum sorting efficiency. The polymer types present in your feedstock directly influence sensor selection: for high-contrast contaminants like aluminum foil or colored paper labels, a machine with advanced color cameras alone may suffice, but for separating black ABS from black PP, you must prioritize near-infrared or laser-based detection modules. The degree of color mixing within your material stream also matters—a flake optical sorter with multiple color channels can handle up to six simultaneous color separations, whereas simpler models may only separate two or three color groups. Throughput needs dictate the sorting width and channel count: a machine with 1,200 millimeter belt width and four chutes processes about 1,500 kilograms per hour of average flake sizes, while doubling the width increases capacity proportionally but requires more floor space and compressed air volume. Oversizing your plastic flake sorter wastes energy and money, but undersizing creates processing bottlenecks that slow entire production lines. Request sample testing from potential suppliers to verify their equipment achieves your target purity thresholds using your actual material mix.
Evaluate sensor technology configurations carefully because combining visible light camera sorting with near-infrared detection generally yields the highest final purity for mixed polymer streams. If your feedstock frequently contains oil-contaminated or wet flakes resulting from improper drying, ask suppliers about special lens cleaning systems that use compressed air blasts or wiper mechanisms to maintain sensor clarity without operator intervention. The choice also should align with your budget and available floor space—some compact models fit into existing production layouts without major structural modifications, while larger industrial units may require reinforced foundations and dedicated ductwork for dust extraction. After-sales support quality can make or break long-term operational success: look for suppliers offering remote diagnostic capabilities that allow technicians to troubleshoot software issues from anywhere in the world, reducing downtime for transportation delays. Local service response times and spare parts availability should influence your decision, as machines with proprietary components may require longer wait periods for replacements. Finally, consider future scalability—a modular plastic flake sorter design allows adding extra detection channels or upgrading sensor arrays as your processing needs evolve, protecting your initial investment against obsolescence. Consulting with industry peers who operate similar machines provides practical insights beyond manufacturer specifications, revealing real-world performance under varying material conditions.
FAQ
What is the maximum flake size a flake sorting machine can handle?
Most flake sorting machines handle flakes from two millimeters to twenty millimeters in their longest dimension. When flakes exceed thirty millimeters, sorting performance typically declines because the detection system struggles to identify consistent color or shape across such large heterogeneous surfaces. Some specialized plastic flake sorter models can accommodate sizes up to fifty millimeters with reduced throughput, as larger pieces require slower belt speeds to maintain accurate scanning. If your process generates oversized shreds, consider installing a pre-screening grizzly or vibratory sieve to remove large particles before they reach the flake optical sorter. The same principle applies to undersized fines below two millimeters, which often escape detection entirely and should be removed separately to prevent contamination of sorted outputs.
Can a flake sorting machine sort black plastic?
Yes, black plastic can be sorted, but it requires specialized sensor technology beyond standard visible light cameras. Black pigments absorb most visible wavelengths, making differentiation impossible for conventional color sorters. However, flake sorting machines equipped with near-infrared (NIR) spectrometers or high-resolution laser sensors can analyze the molecular structure of black plastics and distinguish different polymer types. Advanced models using multi-spectral analysis can even separate black ABS from black HDPE based on subtle differences in their infrared absorption signatures. Before purchasing a plastic flake sorter specifically for black flake applications, always request a test run with your actual black flake mix to verify achievable purity levels. Expect lower throughput rates when sorting dark materials because the detection system requires more processing time per flake to extract meaningful spectral data.
Do I need to prewash flakes before sorting?
Prewashing is strongly recommended for food-contaminated or heavily soiled flakes because moisture, dust, stickers, and organic residues can compromise sensor accuracy. A typical washing line includes friction washers and float-sink tanks to remove labels, glue, and contaminants before the drying stage. For dry, clean post-industrial scrap such as injection molding runners or extrusion trim, prewashing may not be necessary, provided the material remains dust-free. Wet flakes entering a plastic flake sorter can cause water droplets to scatter scanning light, leading to false rejections or missed contamination. Even when prewashing is not required, a de-dusting step using air classification improves detection reliability by eliminating fine particles that might adhere to sensor windows. Understanding your specific material condition helps determine whether washing adds value or unnecessary operating cost.
How often should I clean the optical sensors?
Optical sensors require cleaning every two to four hours of continuous operation in dusty or contaminated environments to maintain detection accuracy. Accumulated dust, plastic fume residues, or fine powder on lens surfaces reduces light transmission to the cameras and distorts spectral readings. Most modern flake sorting machines include automatic blow-off systems that periodically direct compressed air across sensor windows to clear loose particles. Operators should perform visual inspection of sensor glass daily before startup, and scheduled deep cleaning using appropriate optical cleaning solutions should occur weekly. If your plastic flake sorter operates in particularly harsh conditions with sticky organic residues, a spare set of sensor windows allows swapping components for cleaning offline without interrupting production. Establishing a regular cleaning protocol prevents gradual performance degradation that might go unnoticed until product quality falls below specification.